Project Overview
WADJAY-PSC100 CNC flat bar strip bending punching machine: 2T decoiler, 7-roller leveling, 8 gear stations, multi-station hydraulic punch, synchronized cut up to 16m/min, steel/stainless, CE. Get quote.
Why Choose a CNC Flat Bar Punching and Bending Machine?
A CNC flat bar punching and bending machine replaces separate decoiling, manual straightening, stand-alone punch presses and press-brake bending with one coil-fed line. For steel brackets, structural connectors, mounting plates, stainless hardware and automotive/metal fabrication parts, the usual bottleneck is handling: flat coil is uneven, holes are punched offline, bending is reset by hand, and cut length drifts between batches.
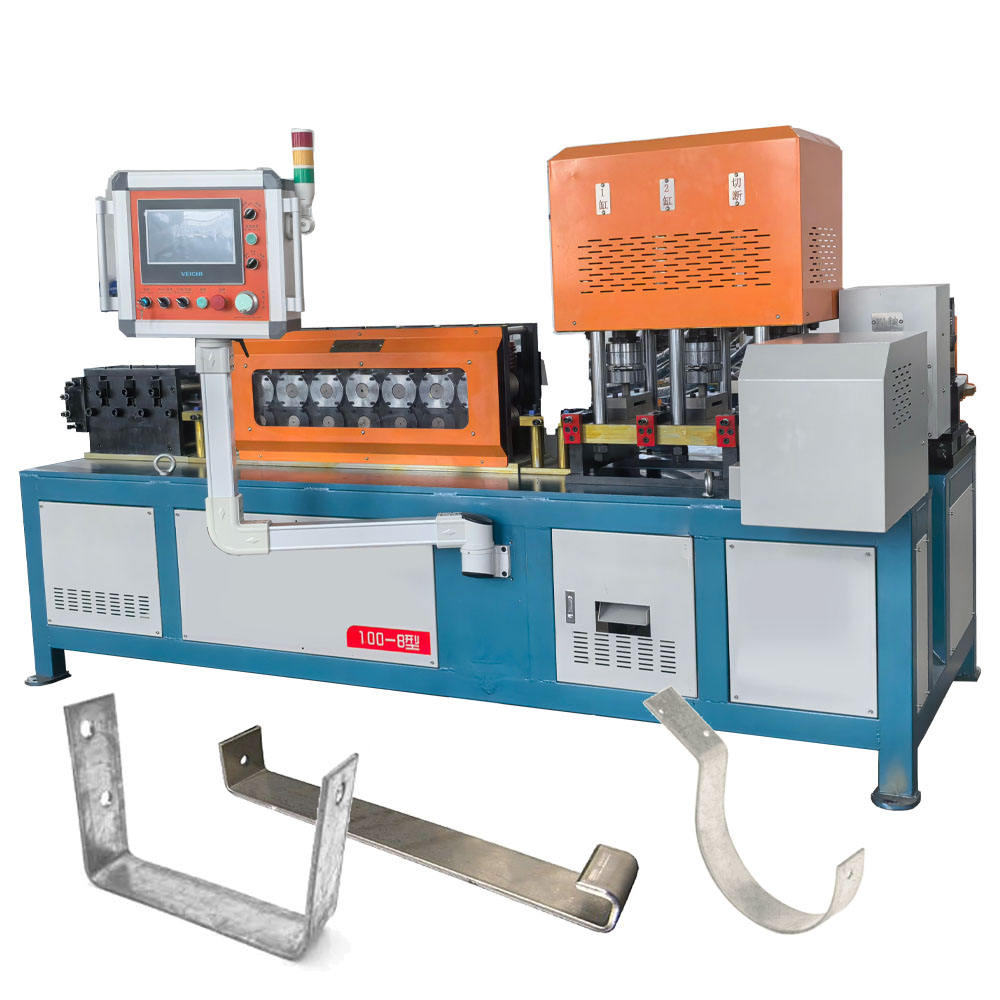
The Wadjay WADJAY-PSC100 runs the full cycle in one CNC loop — heavy-duty decoiling up to 2T, 7-roller straightening driven by a 3.0kW motor, multi-station hydraulic hole piercing, 8 heavy-duty gear-driven forming stands with 4-point independent adjustment, and high-speed synchronized cut-off up to 16m/min. It processes steel or stainless strip into finished brackets/connectors/mounting hardware without moving parts between machines, reducing labor, scrap and setup time.
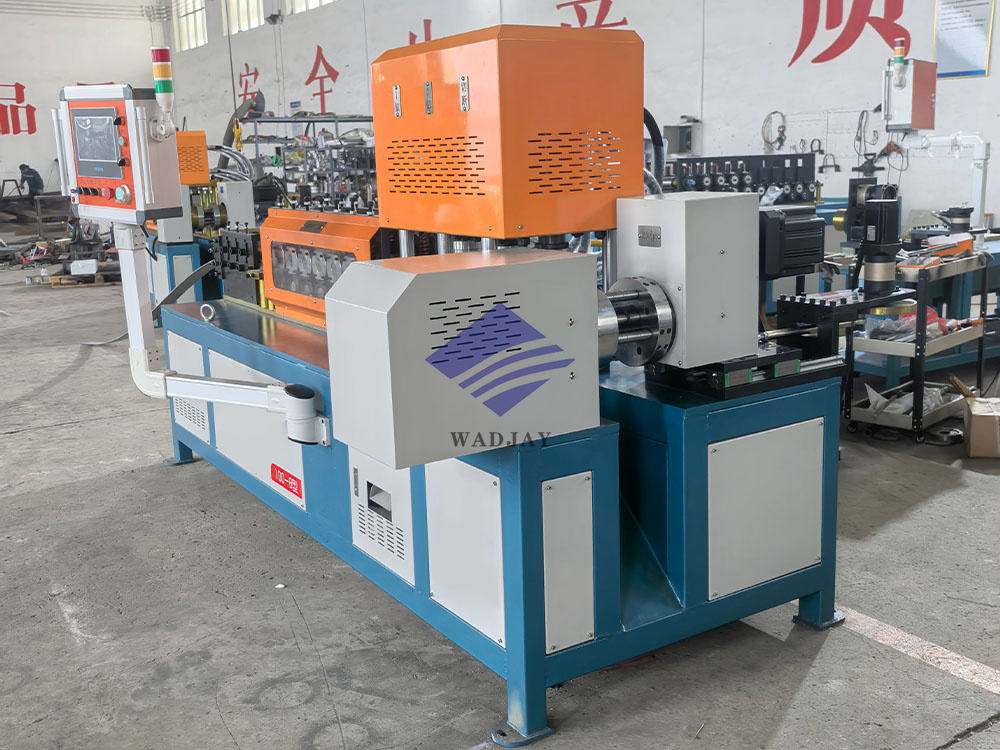
| Module | WADJAY-PSC100 specification |
|---|---|
| Model | WADJAY-PSC100 |
| Process | Decoiling → leveling → CNC feed → hydraulic punching → 8-station gear forming/bending → synchronized cutting |
| Material | Steel strip, stainless steel coil(alloy/aluminum by confirmation) |
| Decoiler | Heavy-duty non-powered/manual expanding pay-off;up to 2T coil load(powered/hydraulic decoiler optional) |
| Straightening | 7-roller arrangement, 4-point independent adjustment;3.0kW drive motor |
| Punching | Multi-station hydraulic piercing for mounting holes/slots/embossing before or during forming |
| Forming | 8 heavy-duty gear-driven stations;progressive bend/shape per profile flower |
| Tension control | 4-point independent roller adjustment to reduce twist/scratch during high-speed feed |
| Cutting | Synchronized cut-off tracked to material feed;burr-free target per blade/tooling |
| Line speed | Up to 16m/min(effective output depends on profile, thickness, hole pattern, bend stages) |
| Control | Smart CNC platform;length/quantity/hole pattern/feed program(PLC brand, HMI language, encoder resolution by configuration) |
| Drive/transmission | Heavy-duty gearbox drive;motor/pump/hydraulic core CE-compliant option;servo/inverter by configuration |
| Strip width/thickness | By profile confirmation(similar Wadjay strip lines reference 30–100mm width, ≤3.5mm decoil/≤2.0mm level;treat as optional, not fixed for PSC100) |
| Shaft/roller material | By configuration(reference options: φ60mm 42CrMo shaft, Cr12/Cr12MoV rollers;confirm per flat-bar profile) |
| Main power | By configuration(reference similar 8-station strip lines 37kW servo;PSC100 document only confirms 3.0kW leveling and gearbox/CNC/ hydraulic modules) |
| Certification | CE-compatible core elements;full CE/ISO documentation configurable by destination |
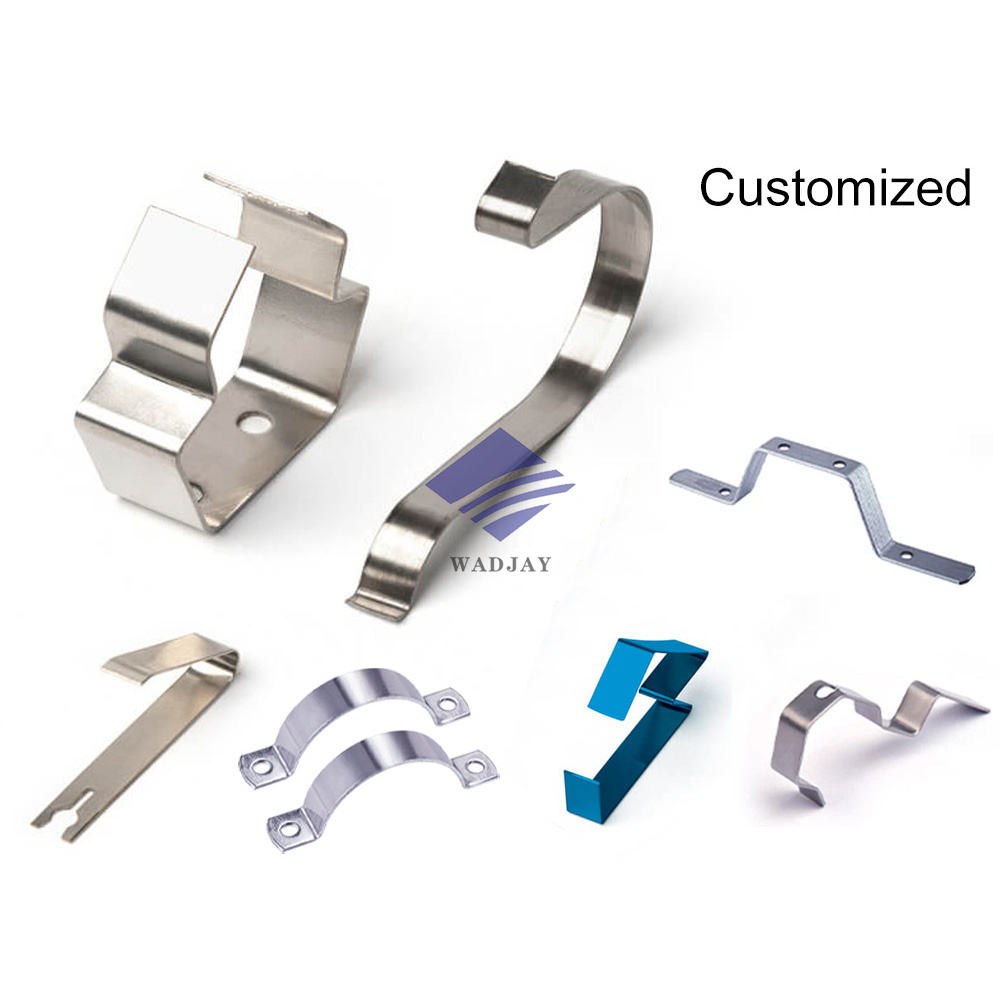
| Output parts | Brackets, connectors, mounting hardware, flat-bar clips, structural/strip components per drawing |
How the PSC100 Flat Bar / Strip Cycle Works
- Decoiling — coil loaded on heavy-duty pay-off reel, manual/non-powered or powered option, up to 2T; strip fed into entry guide without side walk.
- 7-roller leveling — 3.0kW drive plus 4-point independent adjustment removes coil curvature/camber and sets micro tension before punching.
- CNC feed & program — operator inputs strip width, feed length, quantity, hole pitch and bend recipe; encoder/PLC synchronizes each station.
- Multi-station hydraulic punching — mounting holes, slots or embossing pierced in flat or semi-formed state before final bends, so hole-to-bend position stays consistent.
- 8-station gear forming — gear-driven stands progressively bend flat bar into bracket/connector/profile; more stations reduce per-pass deformation and springback for complex bends.
- Synchronized cut-off — shear tracks line speed and cuts finished length without stopping the strip; burr level depends on blade material, clearance and PLC/encoder setup.
- Discharge/stacking — finished brackets/connectors go to run-out/stacking; one operator supervises CNC HMI instead of running press+brake separately.
Application Scenarios
- Structural steel & construction hardware — angle brackets, connector plates, wall/mounting clips, purlin/beam accessories from flat coil.
- Automotive & trailer fittings — flat-bar mounts, strap brackets, punched connector strips requiring repeat hole patterns.
- Electrical & cabinet hardware — DIN/panel brackets, grounding strips, enclosure mounting plates with pierced holes.
- HVAC & duct supports — flat-bar hangers, strap clips, punched mounting flats.
- Stainless architectural hardware — corrosion-resistant brackets/connectors for handrail, facade and equipment mounting.
- Contract fabrication shops — mixed flat-bar profiles reused from CNC recipes, reducing press-brake setup.
Why Wadjay PSC100 Stands Out
- One line instead of press + brake — decoil, level, punch, bend, cut in one CNC cycle; lower manual handling and scrap.
- 7-roller 4-point leveling — 3.0kW drive removes camber/twist before punch, better hole alignment on long strips.
- 8 gear-driven stations — progressive forming for complex brackets/connectors; gear transmission supports stable torque vs chain-only light lines.
- Multi-station hydraulic punching — holes/slots/embossing before bending; consistent pitch for assembly hardware.
- Up to 16m/min sync cut — flying/synchronized cut-off keeps throughput without stopping the strip for standard profiles.
- 2T decoiler + CNC recipes — coil-fed batch production, stored programs for reorder brackets.
- CE-oriented core elements — motor/pump/hydraulic/control selected for export compliance; full CE/ISO docs configurable.
- 24/7 continuous duty option — gearbox, CNC and hydraulic package designed for sustained shift runs subject to cooling/lubrication/service plan.
Related Machines & Internal Links
- Automatic Band Clamp Forming Machine — strip punch/form/cut line for hose/V-band/hoop clamps if buyers also make clamp hardware.
- Pipe Saddle / Cable Cleat Making Machine PSC100 — sister strip hardware line for saddle/cleat/U-strap rather than generic flat-bar brackets.
- C/Z/U Purlin Roll Forming Machine — if the inquiry is for structural channels rather than punched flat brackets.
- Steel Coil Slitting Line — slit wide coil into flat-bar widths before PSC100.
- CNC Press Brake / Shearing — for low-volume irregular flat-bar parts that are not suitable for continuous roll-punch-bend.
FAQs
Q1: What is PSC100 used for?
A: Continuous production of punched and bent flat-bar/strip parts — brackets, connectors, mounting hardware, clips and structural accessories from steel or stainless coil. Send profile drawing for tooling confirmation.
Q2: What strip width and thickness can it run?
A: Documented modules cover steel/stainless strip with decoiling, leveling, punching, 8-station forming and cut. Exact width/thickness depend on profile, yield strength and bend complexity; similar Wadjay strip lines reference 30–100mm width and up to 3.5mm decoil/2.0mm level, but PSC100 values are confirmed per drawing.
Q3: How fast is it?
A: Up to 16m/min synchronized cut under suitable profile, thickness, hole count and bend stages. Effective pieces/min depends on part length, number of bends and punch stations; request a cycle estimate from samples.
Q4: How many forming stations and why 8?
A: 8 heavy-duty gear-driven stations for progressive bending. Complex brackets/connectors with multiple angles or deep returns need more gradual passes to avoid springback, twist or surface marking.
Q5: Does it punch before bending?
A: Yes. Multi-station hydraulic punching can be set before forming for flat-strip holes/slots, or combined with post-form punch per profile. Pre-punch is preferred when hole-to-bend position must stay fixed.
Q6: What leveling and tension control?
A: 7 rollers with 4-point independent adjustment, 3.0kW straightening motor; micro tension control reduces twisting/scratching during high-speed feed.
Q7: What control system and accuracy?
A: Smart CNC/PLC platform for length, quantity, hole pitch and bend recipe; encoder-based sync cut. PLC brand, HMI language, encoder resolution and cut tolerance are configured by destination and profile; do not publish a single fixed ±value without acceptance test.
Q8: What power, shaft and rollers?
A: Gearbox drive with CE-oriented motor/pump/hydraulic core. Shaft/roller/material options (for example φ60mm 42CrMo shaft, Cr12/Cr12MoV rollers on similar lines) are quoted per flat-bar thickness, width and hardness.
Q9: CE, warranty, lead time and price?
A: CE-compatible core elements standard; full CE/ISO export package configurable. Warranty, lead time, installation, commissioning and price depend on width/thickness/profile, punch stations, CNC/hydraulic options, voltage and destination Incoterms.
Q10: How do I request a quote?
A: Send flat-bar drawing (material, width, thickness, yield, hole size/pitch, bend angles/radii, part length, daily quantity, voltage/Hz, PLC preference, CE/ISO docs). Wadjay returns stand layout, punch tooling, roller plan, control/hydraulic option and price.